

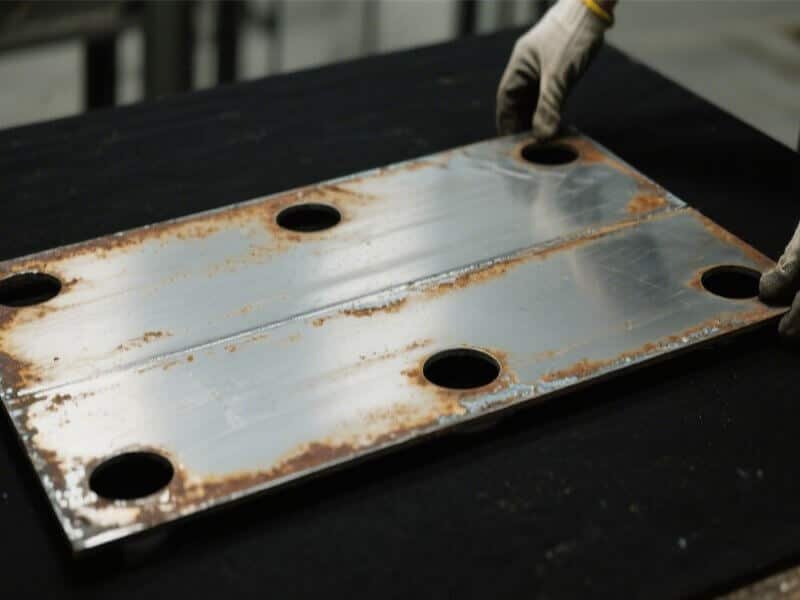
A batch of laser-cut brackets comes off the machine looking perfect: clean edges, tight tolerances, and exactly to spec. Then someone stacks them on a assembly table, and half of them rock back and forth like a seesaw.
That warp wasn’t there before cutting. It showed up because of thermal stress during the cutting process, and now every part needs fixing before it can move to welding or final assembly. This issue happens far more than most buyers expect, particularly with thin gauge sheet or long, narrow parts. The good news is that learning how to flatten sheet metal efficiently isn’t complicated once you understand what causes the distortion.
Key Takeaways
- Laser cutting heats metal unevenly, which is the primary reason sheets warp after cutting.
- Thin gauge sheets and long, narrow parts warp the most because they have less mass to absorb heat stress.
- Manual hammering or torch heating works for one-off parts, but it isn’t reliable for high-volume production runs.
- A dedicated sheet metal leveling machine uses multiple roller passes to apply controlled counter-bending pressure, removing warp without damaging the material.
- When buying a leveling machine, evaluate roller count, precision adjustability, and thickness range.
Table of Contents
Why Does Sheet Metal Warp After Laser Cutting?
Laser cutting heats a narrow strip of metal to extremely high temperatures in milliseconds. Because that heat doesn’t spread evenly across the entire surface, the immediate cut line expands rapidly while the surrounding material remains relatively cool.
This extreme temperature differential creates high internal stress. As the metal cools and contracts, those stressed zones pull against the rest of the sheet, causing it to bow, twist, or cup.
- Material Thickness: Thinner sheets distort more easily because they lack the structural mass to resist thermal pull.
- Part Geometry: Long, narrow components lack multidirectional rigidity, making them particularly prone to bowing.
- Nesting Layout: Cutting parts too close together—or concentrating heavy cuts on one side of a sheet—concentrates heat buildup and amplifies warping.
This distortion doesn’t mean your laser cutter is misconfigured; it’s simply a reality of physics. That is why learning how to properly flatten sheet metal is an essential post-processing step in precision fabrication.
What Does It Mean to Flatten Sheet Metal?
To flatten sheet metal means to permanently neutralize internal stress and eliminate wave, bow, or twist without changing the sheet’s thickness or damaging its surface finish. The end result is a part that lies completely flat with zero rocking motion.
Achieving true flatness is critical for downstream efficiency:
- Automation & Press Brakes: Warped parts won’t index properly against backgauges or feed accurately through automated equipment.
- Welding & Assembly: Distorted components lead to poor fit-up, uneven gaps, and difficult welding setups.
- Final Quality: Left uncorrected, minor sheet distortion carries through to the finished product, where rework becomes exponentially more expensive.
How Does a Leveling Machine Flatten Sheet Metal?
A sheet metal leveling machine uses series of staggered, motorized rollers to work out material tension. As the part passes through the machine, each set of rollers subjects the metal to a series of controlled, alternating upward and downward bends.
Instead of forcing a single harsh bend, this gradual mechanical flexing kneads out the internal stress to flatten sheet metal uniformly.
- Roller Density: A higher roller count allows for smaller, more precise counter-bends, yielding superior flatness on difficult or thin materials.
- CNC Precision: Modern CNC leveling machines automatically adjust roller gap and pressure based on material specs entered into the control panel, ensuring repeatable results across large batches.
- Coil Integration: For continuous coil operations, a Cut to Length Line integrates uncoiling, leveling, and shearing into a seamless workflow so material is perfectly flat before it ever hits the laser cutting table. If the coil requires slitting first, a Slitting Line Machine processes narrower strips prior to final leveling.
Leveling Machine vs. Straightening Machine: What’s the Difference?
While both machines correct material distortion, they serve distinct manufacturing roles:
| Feature | Sheet Metal Leveling Machine | Straightening Machine |
| Primary Material | Flat sheet, plate, and uncoiled sheet metal | Bar stock, wire, tubing, and structural profiles |
| Correction Type | Multi-directional flatness, bowing, and internal stress | Linear bends along a single axis |
| Target Defect | Warping caused by laser cutting or stamping | Curvature from extrusion, drawing, or rolling |
If your primary challenge is fixing surface warp on flat parts after laser cutting, a sheet metal leveler is the correct equipment investment.
Manual Methods vs. Machine Leveling
Smaller job shops frequently try to flatten sheet metal using manual techniques like mallets, heavy presses, or flame heating. While these tactics can work in specific scenarios, they have clear limits:
Manual Methods
- Best For: Low-volume prototypes, one-off custom parts, minor warp, and loose tolerances.
- Drawbacks: Labor-intensive, non-repeatable, skill-dependent, and carries a high risk of adding localized stress or surface heat discoloration.
Machine Leveling
- Best For: Production runs, strict flatness tolerances, thin gauge materials, and automated lines.
- Drawbacks: Requires upfront capital investment.
For high-volume precision fabrication, automated machine leveling is the only way to achieve consistent, repeatable results at scale.
What to Look for When Buying a Leveling Machine
If you are evaluating equipment to flatten sheet metal in your facility, focus on these critical specifications:
- Thickness Range: Ensure the machine’s roller diameter and spacing can accommodate both your thinnest sheets and thickest structural plate.
- Roller Count & Support: Higher roller counts with heavy-duty backup rollers prevent deflection and deliver flatter results on high-strength metals.
- CNC & Programmability: Look for intuitive controls that store job recipes, allowing operators to recall exact roller setups instantly.
- Line Width: Select a working width that matches your standard sheet sizes with comfortable side margin.
- Upstream/Downstream Compatibility: Verify how well the leveler integrates with your existing laser cutting, deburring, or cut-to-length systems.
- After-Sales Support: Choose a manufacturer that offers reliable technical service, fast spare parts availability, and operator training.
Pro Tip: Always Request a Sample Test
Before purchasing a leveling machine, send samples of your actual warped, laser-cut parts to the manufacturer for test runs. Evaluating your own material post-leveling will prove performance far better than a technical brochure.
Following the leveling stage, many fabricators run parts through a Precision Parts Deburring Machine to remove dross and sharp edges created during laser cutting, ensuring clean handling for downstream welding.
Frequently Asked Questions
Q1: Can I flatten sheet metal after it’s already welded into an assembly?
No. Leveling rollers require direct, uniform contact across the flat surface of an individual sheet. Flattening must take place after laser cutting and before any welding or bending operations.
Q2: Does mechanical leveling affect laser-cut edge quality or part dimensions?
No. Leveling applies controlled flex pressure across the flat plane of the metal. It does not alter your laser-cut edge profiles, hole geometry, or overall dimensional tolerances.
Q3: How thin can sheet metal be before leveling becomes risky?
Materials under 0.5 mm require a specialized precision leveler with fine roller adjustments and smaller roll diameters. Standard industrial levelers may crease or distort ultra-thin gauges.
Q4: Is a single pass through a leveling machine always enough?
For light to moderate warp, a single pass is typically sufficient. For severely stressed or heavy-gauge parts, running a second pass with lighter pressure settings often yields the best results.
Q5: Do I need separate machines for processing coil versus individual cut sheets?
Not necessarily. Many versatile leveling lines can process both continuous coil stock and pre-cut sheet parts, especially when integrated into a modular cut-to-length configuration.
Conclusion
Warped material following laser cutting isn’t a defect or an operator mistake—it is a natural, predictable response to localized heat stress. Incorporating a dedicated process to flatten sheet metal eliminates downstream bottlenecks, speeds up assembly, and prevents costly scrap.
If your shop is wasting labor trying to fix warped parts manually, upgrading your workflow with automated leveling technology will safeguard your production efficiency.
Ready to eliminate warped parts?
At iMachine, we design and manufacture high-precision leveling, cut-to-length, and deburring systems built to handle tough post-laser challenges. Contact the iMachine team today to arrange a sample test run with your material!


